Commercial Ozone Generator Factory: A Look Inside Production Standards for Reliable Ozone Systems
2026-10-24
Most buyers of commercial ozone generators focus on specifications like ozone output or power consumption, yet the real story of a reliable system starts much earlier—on the production floor. This behind-the-scenes look at LUFUTATECH’s factory shows how strict production standards, from component sourcing to final testing, separate equipment that lasts for years from units that fail under pressure.
What Happens Before the First Weld: Raw Material Audits and Supplier Vetting
The glow of a welding arc never touches metal that hasn't already passed under a microscope and through a paper trail. Before any torch is lit, incoming coils, plates, and filler wire are sorted by heat number and checked against mill certificates that list exact chemistry, tensile strength, and impact ratings. A batch of 316L stainless that drifts too high in carbon won't just cause porosity; it can crack weeks later in service. So the receiving team slices off small coupons, runs a spectrometer over the surface, and logs the results against the purchase order. If the numbers don't line up, that material gets quarantined before it ever reaches the cutting table.
Supplier vetting is just as deliberate. It's not enough that a vendor claims ISO compliance or points to a glossy brochure. A fabricator's own quality team will visit the mill or service center, walk the floor, and ask to see calibration records for testing equipment. They'll pull random samples from inventory, not the hand-picked showpieces, and send them to an independent lab. One wrong delivery can stall a whole project, so contracts often include the right to audit a supplier's processes twice a year, unannounced. Relationships matter, but so does the right to reject a truckload on the spot if the paperwork or the physical material doesn't match the agreed specification.
This early-stage scrutiny sets the tone for everything that follows. It means welders aren't improvising with unknown alloys or fighting contamination from poorly stored flux. The audit logs become part of the final documentation package, giving the end client proof that every joint traces back to a verified source. Skipping this step might feel like saving time, but it only pushes the risk downstream, where rework costs ten times as much.
Inside the Clean Assembly Bay: Why Controlled Conditions Matter for Ozone Purity
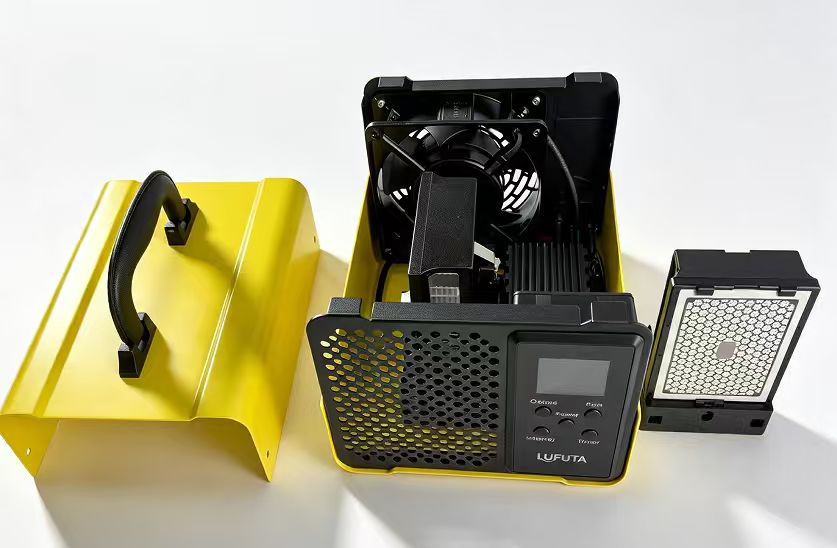
The clean assembly bay isn't just a room with filtered air—it's a deliberate barrier against the microscopic contaminants that quietly compromise ozone purity. Every surface, from the workbenches to the tubing, carries the potential for off-gassing or particulate shedding. When ozone is generated or stored, even trace amounts of hydrocarbons, moisture, or metal oxides can trigger unwanted side reactions, lowering the effective ozone concentration and introducing byproducts that are difficult to remove later.
Maintaining a controlled environment means monitoring more than temperature and humidity. It involves strict protocols for material selection: only ozone-compatible polymers, passivated stainless steel, and lubricant-free fittings are allowed. Personnel move through air showers and wear lint-free garments because a single fiber or skin flake can act as a catalyst for decomposition. The goal is not absolute sterility, but chemical cleanliness—a state where the air itself is scrubbed of volatile organic compounds and the dew point is kept low enough to prevent condensation on internal surfaces.
Why does this matter for purity? Ozone is a highly reactive molecule, and its half-life depends heavily on the cleanliness of its surroundings. In an uncontrolled bay, a freshly charged ozone stream can lose several percent of its concentration within minutes, simply from contact with a slightly oily valve or a plastic hose that wasn't pre-conditioned. The clean assembly bay removes that variability, ensuring that the ozone delivered to the next stage of the process is as close to the generator's output as physically possible—without the silent decay that happens when conditions are left to chance.
Every Unit Gets a Stress Test: Validating Output Under Real-World Loads
Shipping a unit without pushing it past its comfort zone is like handing over a bridge before testing how it behaves in a storm. We don't wait for the field to reveal weak spots; each unit gets deliberately overloaded, not just to failure but through recovery cycles that mirror messy, real-world conditions. The goal is to see how output holds when demand spikes, when inputs arrive out of order, and when the system has every excuse to fall apart. If it survives the worst we can throw at it in the lab, it stands a chance out there.
Validation isn't a checkbox for us—it's a conversation with the hardware under strain. We push voltage rails to their limits, slam data buses with bursts that would make a production environment blush, and watch how the unit's output drifts, dips, or distorts. Then we tune, re-test, and repeat until the behavior under load is predictable. The interesting failures aren't the dramatic ones; they're the subtle changes in timing or noise that only show up when everything is running at once. Those are the ones that get fixed before they become someone's midnight emergency.
What comes out of this process is a unit that doesn't just meet a datasheet—it has a history of surviving the unreasonable. We keep records of every stress profile, every borderline pass, every parameter that shifted under heat or heavy switching. That data shapes not only the final hardware but the next revision. Real-world loads don't follow a script, so neither do our tests. If a unit can't tell the difference between a bad day in the field and a routine bench run, we've done our job.
The Human Side of Production: Training, Cross-Checks, and Error Prevention
On a busy production line, even the most experienced operator can miss a subtle defect when fatigue sets in. That’s why training in modern manufacturing rarely ends after the first week. It evolves into short, scenario-based refreshers where teams review real near-misses and adjust their routines. Cross-checks work best when they feel like a shared habit rather than a box to tick, with a colleague quickly scanning a batch before it moves downstream.
Error prevention, at its core, is less about eliminating human mistakes and more about designing work so mistakes are caught early. One plant I visited paired new hires with veterans for the first month, not just for instruction but for a second set of eyes on every measurement. When a veteran caught a mix-up in raw material labels, it wasn't seen as a failure but as proof that the system worked. Over time, these small checks become instinctive, lowering the chance that a single lapse turns into a costly recall.
The most resilient teams treat training as a conversation, not a one-way lecture. They pause to ask why a step exists and invite operators to suggest simpler, safer sequences. That kind of ownership does more for error prevention than any laminated poster, because people are more likely to follow a process they helped shape.
Tracing a Serial Number Back to Its Birth: Documentation as a Reliability Tool
A serial number is far more than a label stamped on a casing or etched into a frame. It is the first thread of a product's life story. When a component rolls off the line, that number ties it to a specific batch of raw materials, a particular shift of technicians, and a defined set of test outcomes. The documentation attached to that number reads like a birth certificate: alloy composition, heat treatment curves, torque values, and the signature of the inspector who signed off. Years later, when a field failure occurs, an engineer can pull that record and see not just what was built, but exactly how it was built. That turns troubleshooting from guesswork into archaeology, and it stops a single bad part from becoming a fleet-wide mystery.
Consider an aircraft hydraulic valve that starts leaking after 4,000 flight hours. Without traceability, the response might be to replace every valve of that model—an expensive and disruptive fix. With a serial number, the story narrows quickly. The documentation shows that this valve came from a batch where one supplier changed a cleaning solvent without notice. The metallurgical report for that specific heat of stainless steel shows a slightly higher inclusion count. The assembly log notes that a torque wrench was overdue for calibration on that shift. Suddenly, the problem is not "these valves wear out," but "twenty-three units from a single afternoon in March were built under a temporary process deviation." The reliability decision becomes surgical: inspect those twenty-three, leave the rest alone.
Good documentation does more than aid failure analysis—it changes how a company designs for reliability. When every repair, every retrofit, and every teardown result is linked back to the original manufacturing record, patterns emerge that would otherwise stay hidden. One manufacturer of industrial gearboxes noticed that units with a certain bearing supplier had a higher early-life pitting rate, but only when assembled in a specific plant during summer months. That correlation only surfaced because serial numbers connected the dots across separate databases. The fix was not a recall; it was a change to the bearing preload specification and an updated incoming inspection checklist. In this way, tracing a serial number to its birth becomes less about pointing fingers and more about learning from every unit's full journey. Reliability stops being a hope and becomes a recorded, verifiable fact.
Beyond the Factory Floor: Packaging and Pre-Shipment Inspections That Protect Your Investment
Most buyers fixate on what happens at the assembly line, but a product that leaves the factory in perfect condition can still arrive damaged, mislabeled, or packaged in a way that triggers customs delays. That's why shifting attention to the packing floor and loading dock isn't just an extra step; it's where a lot of costly mistakes either get caught or slip through.
Pre-shipment inspections add another layer of assurance after the cartons are sealed and the pallets are wrapped. A third party can verify carton dimensions, shipping marks, barcode legibility, and the actual quantity loaded against your purchase order. Catching a discrepancy at this stage costs far less than discovering it when the container has already crossed an ocean.
Think of packaging and pre-shipment checks as the final gate before your money travels thousands of miles. They help you avoid chargebacks from retail partners, reduce the chance of returns, and keep your cash flow predictable instead of tied up in replacement orders and air-freight scrambles.
FAQ
Look for factories that build around ISO 9001 processes and carry regional safety marks like CE or UL. The real test is whether they document every batch, run ozone concentration checks under full load, and keep calibration records for each unit rather than relying on spot checks.
Reputable lines use calibrated UV absorption or electrochemical sensors to measure ozone concentration at multiple flow rates. They often run each generator for a burn-in period, then compare output against a reference cell. Units falling outside a tight band get reworked or rejected.
Dielectric tubes, electrode coatings, and seals take the most abuse. High-purity alumina or quartz dielectrics hold up better than lower-grade ceramics, while stainless steel or titanium electrodes resist oxidation. Cheap O-rings and gaskets are common failure points, so factories focused on reliability specify fluoropolymer or silicone rated for continuous ozone exposure.
Failures usually trace back to thermal stress, moisture ingress, or substandard dielectric materials. A unit can pass a short bench test but still degrade quickly if the cooling path is marginal or the factory skips humidity cycling. Good production standards include thermal imaging under load and leak-down tests before shipping.
Electrode geometry affects corona discharge uniformity, so consistent gap spacing and surface finish are checked with gauges and microscopy. Factories that invest in CNC-machined electrodes and automated gap verification produce fewer hot spots and longer-lived generators than those relying on hand-assembled parts.
Request a pre-shipment inspection report with serialized test data, not just a certificate. Ask to see failed-unit analysis or if they allow third-party audits. A factory that openly shares calibration logs, material batch certificates, and rework rates is more credible than one that only provides glossy brochures.
Commercial lines typically have dedicated stations for dielectric cleaning, electrode alignment, and automated leak testing. Environmental controls keep humidity low during assembly, and each station logs into a quality management system. Smaller workshops often rely on manual checks that vary by operator and day.
They set statistical process control limits on critical parameters like ozone concentration, power draw, and airflow. If a shift drifts beyond control limits, the line pauses for root-cause analysis. Calibrated reference sensors get rechecked daily or weekly against a primary standard, preventing slow drift from masking real output changes.
Conclusion
Reliable ozone systems rarely come together by accident. Before the first weld is even made, the factory audits raw material suppliers and verifies each batch of stainless steel, ceramic, and sealing compounds for traceability and performance. Inside the clean assembly bay, temperature, humidity, and particulate counts stay tightly controlled because even a small contaminant can compromise ozone purity. Each unit then moves through a stress test that simulates real-world loads, confirming that output levels remain stable when the equipment is pushed beyond typical operating conditions.
Production quality also depends on people. Operators receive continuous training, and critical assembly steps include cross-checks and built-in error prevention so that one oversight does not become a shipped defect. A serial number system allows every generator to be traced back to its raw material lot, test data, and assembly team, which turns documentation into a practical reliability tool. Finally, before a unit leaves the factory, it undergoes packaging and pre-shipment inspections that protect the investment during transit and ensure it arrives ready to perform.
Contact Us
Contact Person: Paul Luo
Email: [email protected]
Tel/WhatsApp: 0086-19966314501
Website: https://www.lufutatech.com