How to Choose a Vision Measuring Machine for Your Quality Control Needs
2026-10-17
Selecting the right vision measuring machine can make or break your quality control workflow—yet many teams still rely on outdated manual checks or settle for systems that can’t keep up. Whether you’re battling tight tolerances, complex geometries, or high-mix production, the stakes are too high for guesswork. This guide cuts through the noise and walks you through the critical factors that separate a precision asset from an expensive paperweight. And if you’re looking for a partner that understands the real-world demands of modern metrology, JATEN has been quietly helping manufacturers turn measurement data into confident decisions.
Start With the Hardest Part You Currently Measure
When you begin with the hardest part you currently measure, you force yourself to confront the metric that already exists but has been quietly avoided. That discomfort is useful. It points to a process or outcome that matters enough to track, yet feels too tangled to improve. Pulling at that thread first often reveals the assumptions baked into the way data gets collected, and those assumptions are usually where the real leverage lives.
A practical move is to name the ugliest number on your dashboard and ask what decision it is supposed to support. If the answer is vague, the measurement itself may be the problem. But if the answer is clear, even a rough improvement experiment becomes possible. You do not need a perfect metric before acting; you need the hardest one you already have, because it has survived contact with reality.
Resist the urge to start with an easy proxy just because it moves quickly. The hard metric rarely gives early wins, but it forces better questions. Once that one is understood, the surrounding numbers tend to make more sense and the next hard part becomes easier to see.
Why a Tiny Field of View Can Beat a Huge Stage
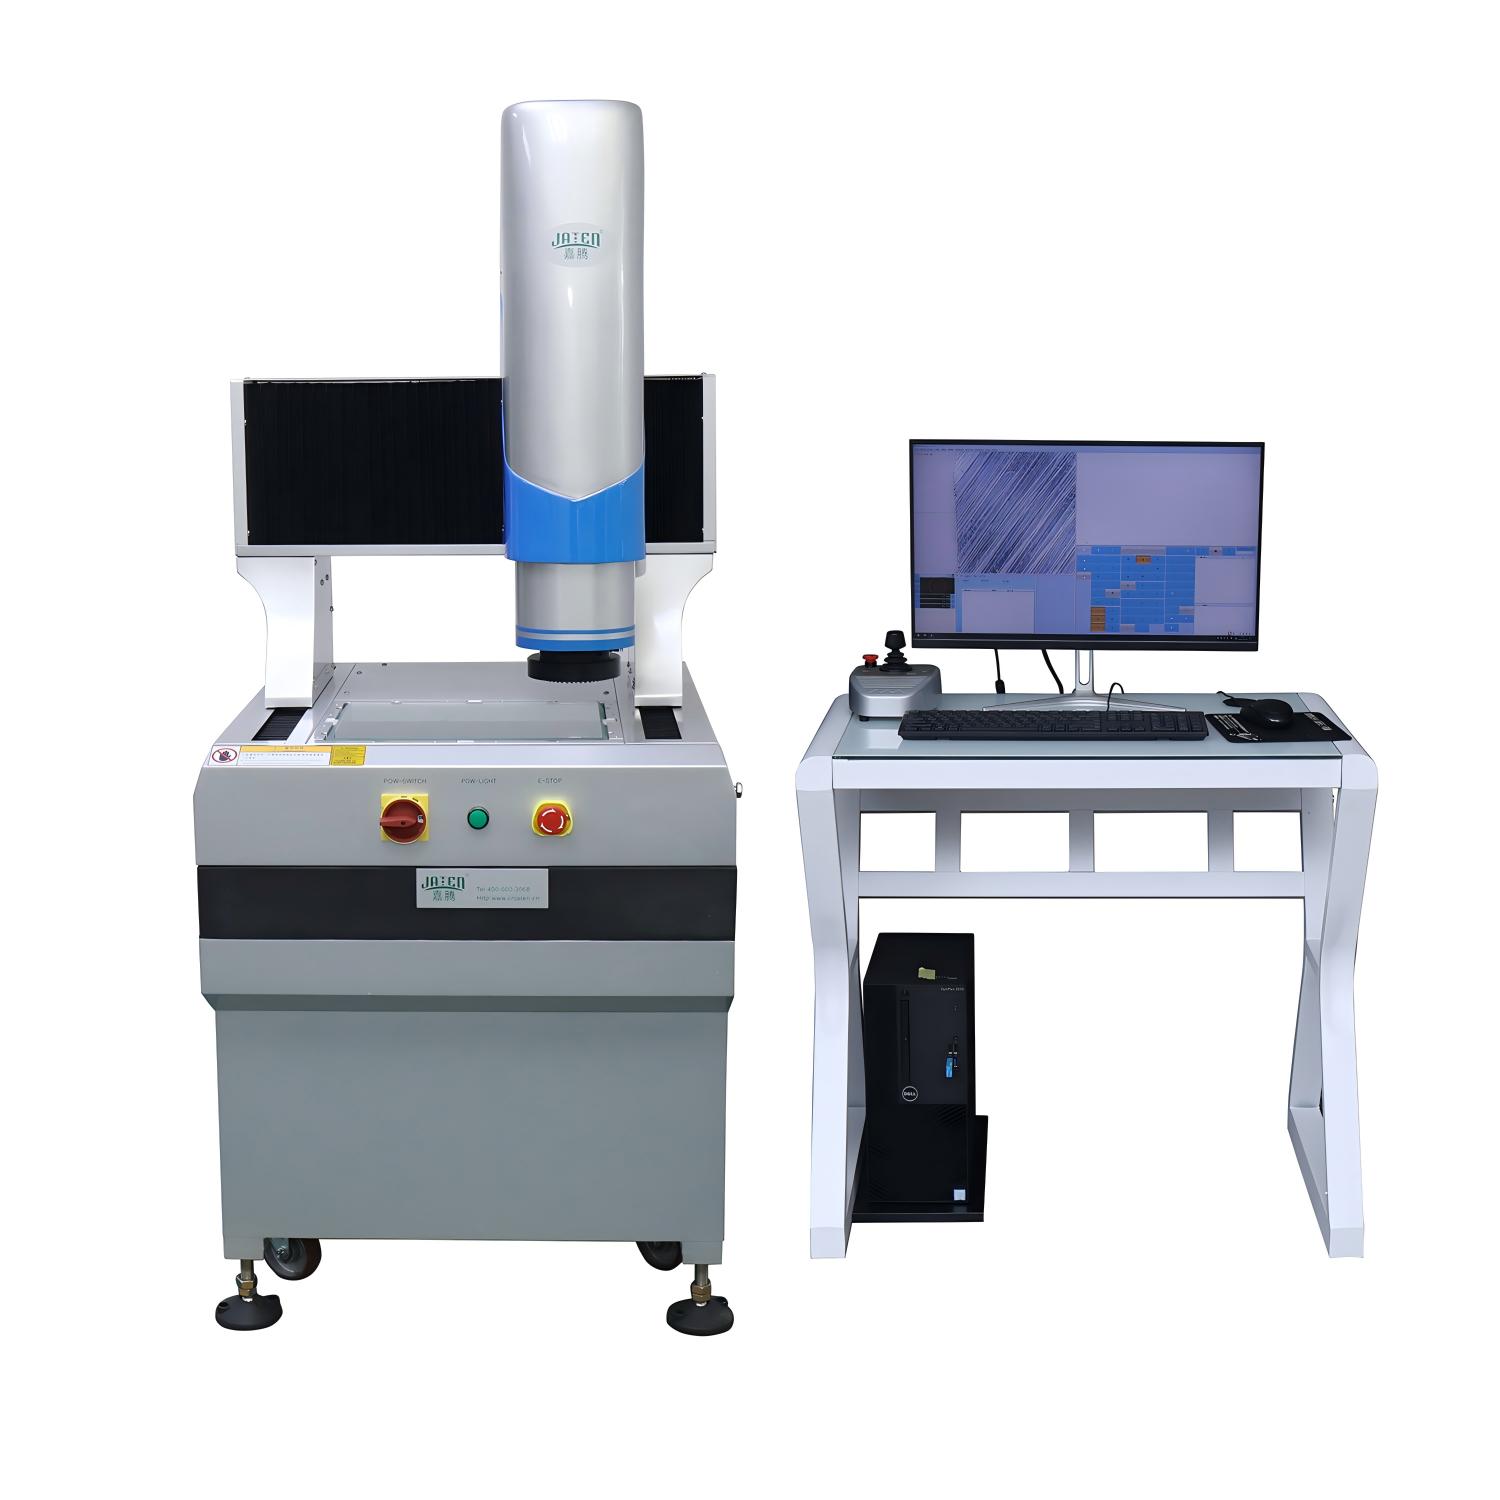
Most performers assume bigger is better — more room to move, more space for spectacle. But a tightly framed camera or a compact stage forces every gesture to earn its place. Without the luxury of wandering or filling empty air, you start to treat each glance, each breath, each half-step as a full sentence. That compression changes your physical vocabulary. A raised eyebrow becomes a plot twist. A hand resting on a table becomes a declaration. The audience leans in because there is nowhere else to look, and suddenly the smallness isn't a limitation — it's a magnifying glass.
Think of how a close-up in film works: the background falls away, the noise of the environment disappears, and all that remains is a face thinking, deciding, hiding, or breaking. A tiny stage can do the same. When you only have a three-foot square to work with, you can't rely on distance to create drama, so you go inward. You work with timing instead of travel, intensity instead of scale. That friction — the visible effort of holding a moment inside a tight frame — reads as authenticity. Audiences don't remember how far you walked; they remember how still you stood when it mattered.
There is also a practical beauty: fewer moving parts, fewer things to go wrong. A huge stage demands filling every corner, which often leads to padding, props, and empty motion. A tiny field of view strips all that away. You become the entire set, the lighting rig, the special effect. And because the audience has less to visually process, they hang on your words with unusual attention. It's not about shrinking your ambition — it's about concentrating it until a single square meter holds more weight than a football field.
The Accuracy Spec Everyone Quotes, and What It Hides
Everyone loves a simple number. Open any datasheet and there it is—the headline accuracy figure, bolded and boxed, promising 0.1% or better. But that single spec is often a best-case snapshot taken under tightly controlled lab conditions, not a promise for your board sitting inside a hot enclosure.
What gets hidden is the fine print. A "0.1% accuracy" might only apply at full scale, meaning a reading near zero could be off by several percent once you account for offset and gain errors. Temperature drift alone can wipe out that headline number unless you're lucky enough to operate at exactly 25°C all day. And then there's long-term stability—specs rarely mention how the device behaves after a year of power cycles and humidity swings.
So before you quote that number in a design review, ask what it leaves out. Check the error budget, the temperature coefficient, the noise floor, and whether the spec is guaranteed or just typical. In practice, the real accuracy is often two or three times worse than the headline—and knowing that early can save a lot of rework later.
Run Your Own Samples Before You Trust the Demo
Demos are built to impress you in the first five minutes. They use curated data, tuned settings, and just enough hand-holding to make the result look effortless. But your real-world samples won't arrive pre-cleaned or perfectly aligned with the vendor's showcase. That's why a quick spin with your own files is the only honest check: if the tool chokes on your messy CSV or misreads your domain-specific jargon, you'll see it within minutes, not after signing the contract.
Don't just drop in one easy file and call it a day. Feed it the odd stuff—the multi-line fields, the irregular date formats, the edge cases nobody thought to include in the slide deck. Watch what breaks and how gracefully it recovers. Then push a sample that's slightly bigger than you'd normally handle, because demos love to hide performance cliffs behind small volumes. If the output still holds up, you've earned some confidence. If not, better to find out now than in a live migration.
Operator Workflow Is the Real Cost Nobody Calculates
When companies audit their expenses, they focus on line items like software licenses, raw materials, and payroll taxes. But the slow bleed often comes from how operators actually move through a shift. Every extra click, redundant confirmation step, or manual data re-entry pulls seconds away from core work. Those seconds compound across stations, shifts, and facilities into a hidden tax that never appears on a balance sheet.
Consider a packaging line where operators must toggle between three separate systems to log a single batch. The official cycle time says ninety seconds, but the real-world workflow takes four minutes. Managers blame fatigue or training, yet the system itself forces the detour. No individual error causes the loss; the accumulated friction does. Once you map the true sequence of actions, the cost becomes impossible to ignore.
The fix rarely requires new machinery. Often it means removing a confirmation dialog, pre-filling a field, or letting one scan replace two. Operators already know where the workflow hurts. The companies that ask them, watch them, and then eliminate the friction are the ones that stop paying for work that doesn't actually move product forward.
Leave Room for Fixtures, Data Export, and Next Year's Parts
When you lay out a new workspace, the temptation is to fill every drawer, rack, and shelf with exactly what you need today. That approach works until a customer sends an unexpected fixture, a new test jig arrives, or you discover that the original setup blocks access to a critical port. Leaving open space near the active work zones means you can slide in a fresh fixture without moving half the bench or drilling new holes in the wall.
Data export rarely gets the same forward planning. A clean schema or a tidy folder structure feels finished, but someone downstream will eventually ask for a batch extract, a nightly sync, or an archived snapshot in a format you never considered. If your current layout assumes a fixed export path or a hard-coded file name, you will spend an afternoon untangling that choice instead of shipping the data. Build in a few empty fields, a generic staging directory, or a version column now, and the next export request becomes a configuration change rather than a rebuild.
Next year's parts will not be identical to this year's. Suppliers revise tolerances, connectors move from one side to the other, and a simple bracket gains a mounting boss or an extra cable clip. A rack designed to hold only today's exact dimensions becomes a liability the moment the revision lands. Keep the mounting holes slotted, leave a little slack in the wire runs, and store one or two untapped bracket positions. The extra room costs nothing during assembly but saves you from tearing apart a supposedly complete system when the updated components finally show up.
FAQ
Start with the measurement envelope and the type of parts you actually inspect. A system that can't physically hold your largest component or reach all critical edges is useless no matter how accurate it is. Write down the maximum length, width, and height you need, then add about twenty percent headroom. Also note surface finishes: highly reflective, matte, or textured parts each place different demands on optics and lighting, so one-size-fits-all thinking often leads to failed measurements on the shop floor.
Let your inspection volume and operator skill guide that call. If you're checking a handful of parts per day and your team is comfortable aligning stages by hand, a manual machine keeps costs down and works fine. Once you run dozens of parts per shift or need repeatable positioning without relying on one skilled person, move to CNC or semi-automatic control. A fully automatic system pays off when you have batch runs, multiple fixtures, or want operators to load a part and walk away while the machine measures and logs everything.
Because the best lens in the world cannot measure an edge it can't see clearly. Different parts need different illumination: backlighting works well for outer contours, while ring or coaxial lighting handles holes, steps, and surface features. If the lighting is fixed or weak, you'll waste time adjusting part placement and still get unstable readings. Look for machines that let you save lighting programs per part number, because switching between shiny, dark, and translucent materials is far easier when illumination settings are stored rather than recreated from scratch each time.
Ignore the single impressive number on a brochure and ask about volumetric accuracy at the working plane, not just resolution. Repeatability matters more than resolution because a machine can display four decimal places without being able to return to the same point twice. Ask the vendor how the stated accuracy was tested, at what temperature, and over what travel range. Then request a simple gauge R&R or a test measurement on your own part. A machine that holds a few microns on your actual component beats a spec sheet full of lab-only figures.
Software is where operators spend ninety percent of their time, so if it feels clunky during a demo, it will feel worse at 4 p.m. on a Friday. Look for a clean interface that lets you create a measurement routine in minutes, not days. Features like one-click edge selection, drag-and-drop reporting, and tolerance highlighting reduce human error. Also check whether the software exports data in the format your quality team already uses. A beautiful hardware system paired with awkward software often leads to people avoiding the machine and going back to hand tools.
Vision measuring machines are less forgiving than regular hand tools. Vibration from nearby presses, temperature swings near loading docks, and uneven floors can degrade accuracy quickly. Check the machine's required operating temperature range and whether your area stays within it through all seasons. You may need a dedicated bench, isolation pads, or a climate-controlled room. Lighting from windows or overhead fixtures can also interfere, so plan for shades or a booth. Sorting out these basics before delivery avoids a painful period where the new machine measures worse than your old manual method.
A vision measuring machine is not a buy-it-and-forget-it tool. Ask about calibration intervals, whether the vendor offers on-site service, and typical response times. You want a clear path for annual verification against certified standards, plus access to software updates that fix bugs without breaking existing routines. Talk to local users if possible; a vendor who disappears after installation leaves you stuck when a stage motor fails or a lighting controller acts up. A slightly more expensive machine with dependable local support often costs less over five years than a bargain unit with no backup.
Separate must-haves from nice-to-haves before you talk to salespeople. If your parts are flat stampings, a high-end rotary indexer or laser autofocus may be wasted money. But don't cut so close that a new product line forces a full replacement. Choose a platform that lets you add probes, a larger stage, or a better lighting module later. This modular approach costs a bit more up front but keeps the machine useful when your inspection tasks expand. The goal is to buy enough capability to handle realistic future work without funding a laboratory toy in a production environment.
Conclusion
If you are trying to pick a vision measuring machine, do not start by comparing brochures. Start with the part that currently gives your inspectors the most grief—the one with the tightest tolerance, the trickiest edge, or the feature that takes forever to set up. A machine that can handle that difficult part without a struggle will usually sail through the easy ones. That simple shift in focus beats any spec-sheet war. Once you know your hardest measurement, you can judge whether a small field of view actually works better than a giant stage. Big stages look impressive, but if the optics are not sharp where you need them, you are just moving a blur around. Often a compact, high-resolution field of view is faster and more repeatable for the features you actually check.
Be suspicious of the accuracy number everyone quotes on the first page. That figure usually assumes perfect temperature, perfect part, and perfect alignment—not your shop floor at mid-afternoon on a Thursday. Ask for a demo with your own parts, not the vendor's polished samples. Run ten or twenty pieces and watch how long it takes a real operator, not an applications engineer, to load, measure, and export data. The operator workflow is the hidden cost—if every measurement requires five mouse clicks and a prayer, you will lose more money in labor than you saved on hardware. Also leave room for fixtures, data export to your quality system, and parts you have not designed yet. A machine that cannot grow with your next project is just a short-term rental.
Contact Us
Contact Person: Volien
Email: [email protected]
Tel/WhatsApp: +86 18029161762
Website: https://www.jatentech.com/