Ultrasonic Bubble Sensor Supplier Evaluation Tips for Engineers and Buyers
2026-09-23
Selecting the right ultrasonic bubble sensor can make or break your fluid management system, yet too many engineers and buyers still rely on generic checklists that miss critical real-world pitfalls. Whether you're dealing with aggressive chemicals, tight tubing tolerances, or high-throughput production lines, the difference between a reliable sensor and a costly field failure often comes down to supplier evaluation. That's why we've put together these practical tips—drawing on insights from Siansonic's decades of ultrasonic sensing expertise—to help you ask the right questions before you commit. No fluff, just the supplier criteria that matter when downtime isn't an option.
Cutting through vendor demos: questions that expose real bubble sensitivity limits
Most vendor demos are polished to the point of being useless for real-world evaluation. The bubble chart glides smoothly, the sliders respond instantly, and the sensitivity analysis never breaks a sweat. But ask the vendor what happens when two correlated inputs move in opposite directions at the same time, and you’ll often get a blank stare. That’s where the real limits hide. Instead of accepting the canned scenario, push for a live test with distorted distributions, missing data, or non-linear interactions. If the model can’t handle a skewed input without collapsing, your risk team needs to know now — not during a stress event.
A sharper question is to ask how the bubble boundaries were calibrated in the first place. Were they derived from historical data that conveniently matches the demo period? What happens if the correlation regime shifts, or if volatility spikes in one corner of the portfolio? Demos rarely show the edge cases because the vendor knows those are where the cracks appear. Request a walkthrough of a failed backtest, or a scenario where the bubble sensitivity limit was breached. The silence that follows is often more informative than the slide deck.
Finally, watch for the demo’s unspoken assumptions about data quality and timing. Many models assume daily updates, clean feeds, and liquid markets. Ask what happens when a key input arrives late, or when a counterparty stops reporting. If the vendor can’t show you the system’s behavior under those conditions, you’re not seeing a tool — you’re seeing a marketing story. The real bubble sensitivity limit is usually not a number on a chart; it’s the point where the model quietly assumes the world is simpler than it is.
Fluid acoustics beyond the datasheet: viscosity, temperature, and particulate interference
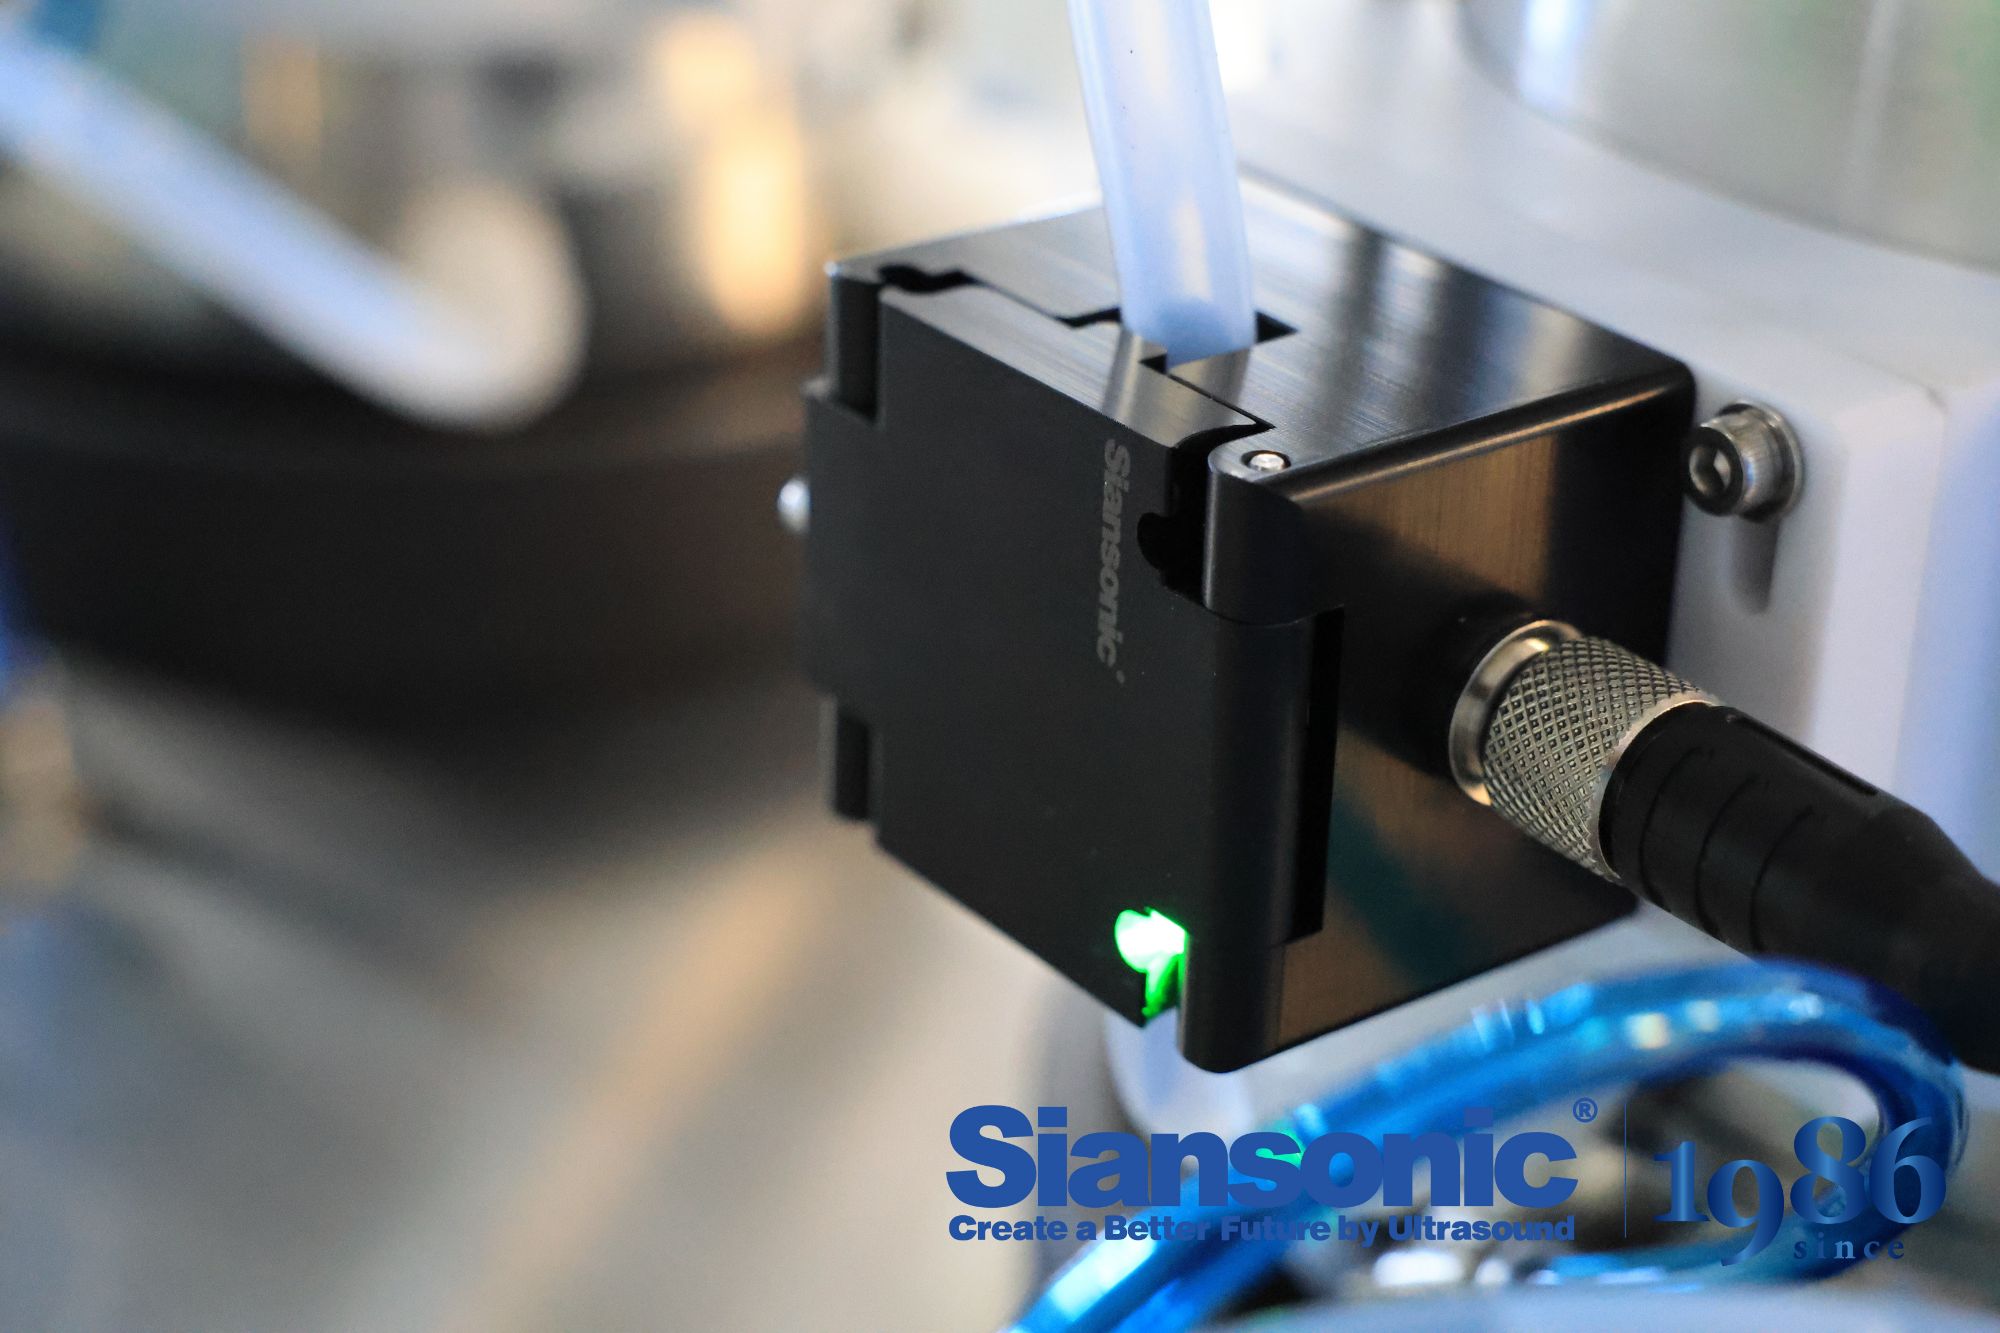
The datasheet for an acoustic flow sensor often paints a clean picture: a specified viscosity range, a narrow temperature band, and an assumption of particle-free media. Real process fluids rarely cooperate. In water treatment lines, for instance, viscosity can swing sharply with seasonal temperature shifts or chemical dosing, while suspended solids—from rust flakes to polymer flocs—continuously scatter and attenuate ultrasonic signals. Operating outside the comfort zone of the datasheet forces engineers to reinterpret raw time-of-flight readings, because the acoustic impedance mismatch at the pipe wall changes with both fluid density and sound speed, neither of which follows a simple linear trend.
Temperature adds another layer of subtlety. Beyond altering viscosity, it shifts the resonant frequency of piezo transducers and deforms the acoustic lens materials, introducing phase errors that look deceptively like flow turbulence. A sensor calibrated at 20°C may read low by several percent at 5°C not because the flow changed, but because the acoustic path length contracted and the transducer’s electromechanical coupling drifted. The fix is rarely a single offset constant; it demands either multi-point temperature compensation or a live reference path that measures sound speed in the same fluid.
Particulate interference is the most insidious. Bubbles and solid particles act as moving scatterers, creating Doppler sidebands that can be mistaken for velocity fluctuations. High particle loads also increase acoustic attenuation exponentially with frequency, forcing designers to drop to lower MHz ranges where spatial resolution suffers. The practical solution often involves a hybrid approach: combine a wideband acoustic burst with digital matched filtering to reject slow-moving particulate echoes, while simultaneously monitoring signal amplitude and spectral centroid as proxy indicators of suspension stability. Only by accepting that the datasheet is a starting point, not a boundary, can field instrumentation stay robust when the fluid refuses to behave like a calibration standard.
Mounting geometry and acoustic dead zones: why placement changes everything
A loudspeaker driver or a microphone capsule rarely behaves the same once it leaves the test bench. The same transducer can measure ruler-flat in an infinite baffle, then show a 6 dB dip at 400 Hz after being bolted into a wall plate. That shift isn't a defect in the component; it's the mounting geometry redefining which reflections arrive in phase and which ones cancel. A surface only a few centimeters away creates a quarter-wave null for a specific band, swallowing detail that was clearly present moments earlier.
Dead zones appear when the direct wave meets a delayed copy of itself from a nearby boundary or enclosure edge. At the frequency where that delay equals half a wavelength, the two signals invert and tear a notch into the response. Microphones suffer the same effect in reverse: a capsule placed too close to a tabletop loses the upper midrange to phase smear, while one mounted flush against a wall gains boundary loading but loses the spatial cues that off-axis placement would deliver. Even the shape of the cut-out around a ceiling speaker dictates whether the lobe points at the listening area or dumps energy into a closet.
Placement changes everything because the distance from the transducer to every hard surface is a tunable parameter. Moving a wall-mounted speaker forward by ten centimeters can move a cancellation dip from 800 Hz down to 250 Hz, or turn a muddy vocal into an intelligible one. There is no universal fix, only a map of nulls and peaks tied to the geometry of the room and the mounting hardware. Until you trace those reflections, you are not tuning the speaker; you are tuning the distance between the speaker and its own shadow.
From golden sample to production run: consistency checks most buyers skip
A golden sample gets approved, and everyone assumes the factory will replicate it perfectly. That assumption falls apart the moment tooling wears down, raw material batches shift, or a new shift operator tweaks a setting without documenting it. Smart buyers don't just compare the first article to the sample; they build a bridge between approval and mass production by locking in measurable parameters—weight, hardness, seam tolerance, color code—and auditing those numbers at fixed intervals, not just at final inspection.
Most skipped checks happen in the messy middle: after pilot run but before full packaging. Pulling random units from the line at hour three and hour seven often reveals drift that a single pre-shipment inspection misses. If you're not asking for those mid-run measurements, you're effectively approving a prototype and praying for a production run.
After-sale support that actually matters: calibration, firmware, and spare part lead times
Calibration is where many suppliers quietly drop the ball. You buy a precision instrument, it arrives well within spec, and then six months later you're chasing ghosts in your measurements. A support program that actually matters won't make you beg for a calibration procedure or wait weeks for a technician. It gives you the reference standards, the step-by-step tolerance checks, and a realistic schedule for when recalibration is genuinely needed—not just when the warranty expires. If they can't tell you how to verify accuracy on your own shop floor, that's a red flag.
Firmware updates should never feel like a gamble. Too many vendors push out patches without clear release notes, leaving you to discover that a new version broke a workflow you relied on. Solid after-sale support means firmware that arrives with a changelog, a rollback path, and a quiet window to test it before it touches production. It also means not bundling critical bug fixes behind a paid support tier. If your device is going to run for five years, the vendor needs to commit to maintaining that codebase for five years—not just until the next model ships.
Spare part lead times are the least glamorous part of support, but they'll shut you down faster than any other issue. A quoted "2-3 weeks" for a replacement board can turn into two months of downtime if the vendor doesn't actually stock the part. The vendors worth keeping are honest about what sits on their shelf versus what gets drop-shipped from a contract manufacturer. They'll tell you which components are wear items, keep those in local depots, and offer an expedite path that doesn't require a purchase order battle. Real support means you can plan maintenance around part availability—not plan your production around the courier's mood.
Total cost per detected bubble: looking beyond the unit price
When evaluating bubble detection systems, the sticker price per unit often grabs all the attention, yet it rarely reflects what you actually pay once the technology is integrated into a live production line. Maintenance visits, calibration drift, false-positive rates that trigger line stoppages, and operator retraining all quietly pile onto the initial purchase. A detector that looks cheap on paper can become the most expensive option if it demands weekly recalibration or flags harmless micro-foam as defects, slowing throughput to a crawl.
The real metric is the total cost spread across every bubble genuinely caught and correctly classified. This includes not only hardware depreciation and sensor replacement, but also the labor hours spent verifying alarms, the lost yield from mislabeled rejects, and the energy overhead of running high-intensity lighting or pressurized inspection chambers. Some facilities find that a mid-priced system with smarter image processing dramatically lowers cost per detected bubble because it needs fewer manual reviews and keeps the line moving at full speed.
Procurement teams should therefore request a cost-per-detection model from vendors rather than a simple quote. Ask for data on false rejection rates, mean time between failures, spare part longevity, and how often the software needs retuning for different container shapes or liquid viscosities. Only when these operational expenses are folded into the calculation does the true economic picture emerge, and often the unit price that once seemed unattractive becomes the clear winner on the floor.
FAQ
Start with bubble detection threshold, which should be specified for the exact tubing diameter and material you use. Check the response time under varying flow rates—some sensors lag when liquid moves faster than 200 ml/min. Repeatability across temperature shifts is also critical, because readings can drift if the supplier has not compensated for acoustic impedance changes.
Ask for application notes or case studies that name specific fluids, viscosities, and tube wall materials. A genuine manufacturer will freely discuss transducer design, drive frequency choices, and how they handle air-in-line versus micro-bubble detection. If they cannot explain calibration procedures for non-invasive clamp-on sensors, that is a warning sign.
Request the full data sheet with tolerance ranges, not just typical values. Ask for a documented PFMEA or control plan for the sensor assembly, including transducer bonding and potting. Batch traceability and incoming inspection reports for piezoelectric elements reveal how seriously they treat consistency.
Low-cost sensors often lack built-in temperature compensation or have wide detection thresholds, causing false alarms in real systems. You end up paying for extra filtering circuits, frequent recalibration, or field returns. A slightly higher unit price usually buys better repeatability and lower total cost of ownership.
Build a simple test loop with the actual tubing and fluid, then inject controlled air bubbles using a syringe pump. Measure how consistently each sensor detects 50-microliter versus 200-microliter bubbles at three different flow rates. Run the test for at least 48 hours to catch drift or false positives.
For medical or pharmaceutical applications, ISO 13485 certification and FDA master file support are non-negotiable. You also need documentation for biocompatibility of wetted materials if the sensor contacts fluid. An industrial supplier may offer a lower price but cannot provide the design history file you need for your own product approval.
Find out whether the sensor is clamp-on, inline, or requires a custom housing. Ask about recommended tube durometer and wall thickness tolerances—ultrasonic coupling depends heavily on these. Also confirm the output type: analog voltage, digital threshold, or I2C, and whether the supplier provides reference firmware for your microcontroller.
Ask for references from customers who have used the sensor for at least two years in a similar environment. Check how quickly the supplier responds to technical questions during the evaluation phase; slow pre-sale support often predicts worse post-sale support. Also confirm their policy on firmware updates and whether they offer failure analysis reports if sensors fail in the field.
Conclusion
When sitting through vendor demos, don't let a crisp air bubble in room-temperature water convince you the sensor will work in your line. Ask for the smallest detectable bubble size at your actual flow velocity and pressure, and whether that threshold holds over hours, not just during a two-minute demo. Fluids in production rarely match the lab: higher viscosity attenuates ultrasonic signals, temperature swings change acoustic impedance and sound speed, and suspended particles can trigger false positives or hide real bubbles. Datasheet numbers often come from idealized conditions. Before you sign anything, test the sensor with your own tubing, including the exact inner diameter, wall material, and any bends or reducers near the measurement point. Mounting geometry creates acoustic dead zones—areas where bubbles pass through but the sensor stays blind—especially close to transducer faces or directly after a sharp elbow. Repositioning the sensor by a few centimeters can be the difference between reliable detection and missing every bubble in a critical line.
The golden sample the supplier sends has likely been hand-picked and fine-tuned, so it tells you little about what you'll get in a bulk order. Request a production-run sample or at least run a small pilot with five to ten units, checking threshold drift, baseline noise, and response time consistency. Many buyers skip this step because it takes time, but unit-to-unit variance is where hidden costs creep in. Ask direct questions about after-sale support: is field calibration possible or must sensors be returned? How often is recalibration actually needed in your fluid? Are firmware updates user-installable or factory-only? What is the realistic lead time for replacement transducer assemblies if one fails on a Friday night? Finally, don't compare invoice prices. Calculate total cost per detected bubble over the sensor's expected service life. A low unit price that comes with high calibration burden, frequent false alarms, or a six-week spare part lead time can easily wipe out the initial savings. The right supplier evaluation weighs real-world performance, support responsiveness, and long-term reliability—not just the number on the quote.
Contact Us
Contact Person: Ivy Zhang
Email: [email protected]
Tel/WhatsApp: +86 1081502288
Website: https://www.siansonic.com/