Why Choose a China Leveling Casters Factory for Your Equipment Needs
2026-08-29
When your equipment demands stability, smooth mobility, and long-term durability, the choice of leveling casters can make or break performance. For many businesses, sourcing from a specialized China leveling casters factory offers a compelling balance of cost efficiency and engineering precision. At CMCL, we combine advanced manufacturing with rigorous quality control to deliver casters that handle uneven floors and heavy loads without compromise. But what exactly sets a dedicated factory like ours apart from generic suppliers—and how does that translate into fewer headaches and better ROI for your operations? Read on to explore the key reasons global buyers are turning to China's expert caster manufacturers.
Matching Your Equipment’s Footprint, Not Just Its Weight
A fifty-pound portable generator and a fifty-pound squat rack couldn't be more different once they're inside your space. The generator tucks into a corner, while the rack demands a dedicated zone with clearance on all sides. Weight tells you how many people you'll need for unloading—it says almost nothing about whether the equipment will dominate your room or leave room to work.
Before comparing specs, sketch the actual footprint on your floor with tape. Include the space needed to open doors, extend arms, or slide out trays. Some machines list only the base dimensions but need an extra two feet behind them for cables or ventilation. If you're tight on square footage, a heavier unit with a vertical design can often be a smarter pick than a lighter one that sprawls.
Also think about how the equipment moves through your building. Doorways, elevators, and stair landings don't care how much something weighs on paper—they care about width and pivot radius. A compact footprint means little if the item can't reach the room where it will live. Checking the path first saves you from the frustration of a machine that fits perfectly on paper but not in practice.
Direct Feedback Loops When Thread Pitch or Wheel Hardness Needs a Change
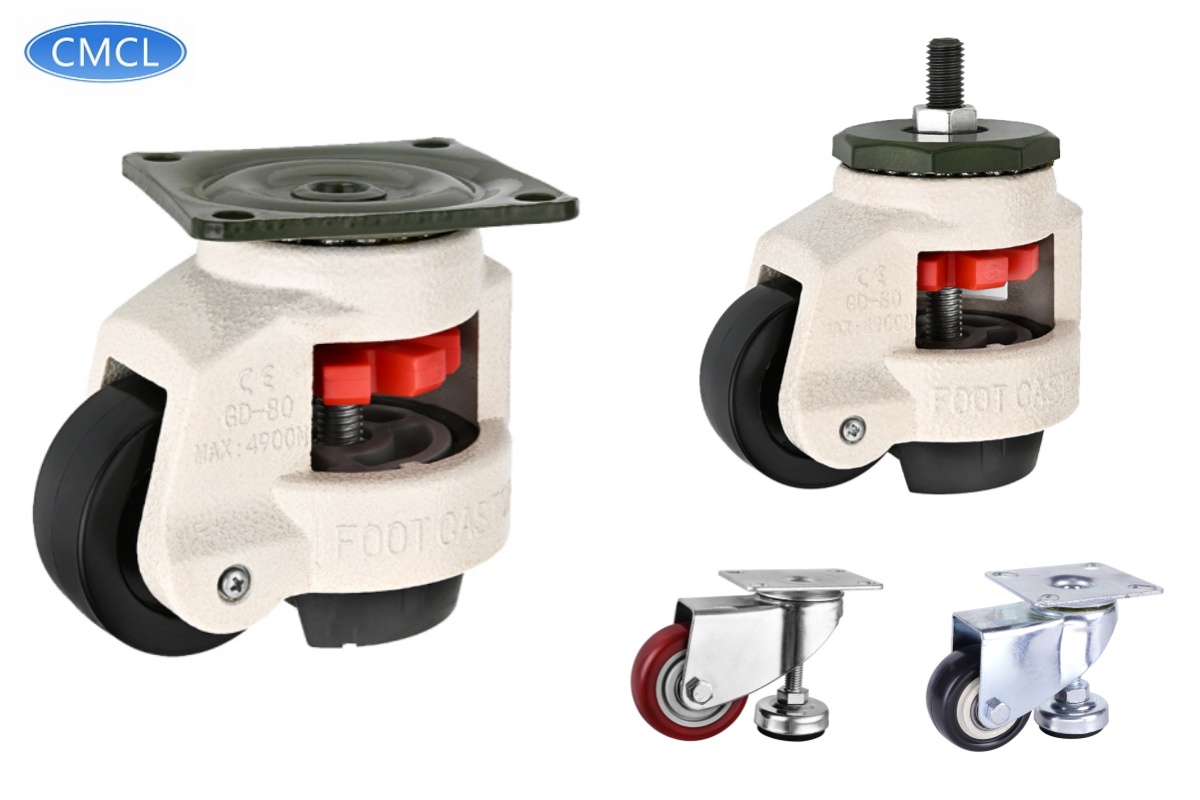
Adjusting thread pitch on a fastener or swapping out a wheel for a different durometer isn't just a tweak—it's a conversation with the machine. When the pitch is too coarse, you feel it immediately: vibration rises, torque curves spike, and the joint settles differently. That's the loop talking. You change the pitch, run a test cycle, and the torque-angle signature shifts in real time. No waiting for a report or a dashboard refresh. The feedback is physical, immediate, and often loud enough to hear before you see the numbers.
Wheel hardness plays the same game but with a softer voice. Go too hard and the surface grip changes, heat builds at the contact patch, and wear patterns start telling stories. Swap to a softer wheel and suddenly the same feed rate feels different—quieter, more compliant, but maybe leaving more debris. The loop here is tactile and visual. Operators read the surface finish, listen for chatter, and check edge rounding on the fly. It's not about a spreadsheet; it's about paying attention to what the process is trying to say.
The real trick is closing that loop deliberately. Write down what changed, what you felt, and what the next adjustment should be. Too often teams swap a wheel or change a pitch, see a marginal improvement, and move on without capturing the cause-and-effect. A direct feedback loop only works if you acknowledge the signal, respond with a single variable change, and watch for the counter-signal. Otherwise you're just guessing with extra steps.
Leveling Pads That Hold Position on Sloped or Worn Floors
Most leveling pads slip the moment a floor tilts or loses its grip—but these don't. The base is lined with a dense, rubberized tread that bites into concrete, tile, or scuffed hardwood without marring the surface. Even on a ramp-like slope or a floor worn smooth by years of traffic, the pad stays exactly where you set it.
Instead of relying on friction alone, the design includes a low-profile locking collar that tightens against the threaded stem. Once you dial in the height, the collar prevents any micro-rotation from vibration or lateral pressure. That means a table leg, machine foot, or appliance corner won't wander downhill or settle into a low spot overnight.
For floors with uneven wear patterns—like a warehouse aisle or an old kitchen—the pad's swivel head compensates by hugging the contour under load. You get level support without shims, and no need to re-adjust every few weeks. It simply holds position, even when the floor beneath it can't.
Mixing Low-Profile and Heavy-Duty Models in One Order Without Delay
Combining low-profile and heavy-duty units in a single purchase used to mean accepting a longer wait. The typical problem is that these two categories often sit in different warehouse zones, with separate picking paths and packaging stations. A simple but effective fix is to assign both models a shared picking wave identifier. When an order enters the system, inventory is checked simultaneously for both types and routed to a common staging area before the cutoff time. This keeps the low-profile items from lingering while the heavier ones are still being located.
Another layer that removes delay is pre-kitting common components. Many low-profile and heavy-duty models share base plates, mounting bolts, or rail adapters. By pre-assembling these shared parts into neutral kits, the warehouse team can grab one kit per unit regardless of profile. The only variable left is the frame or housing, which is already stored in the forward pick zone. This reduces the time spent walking between distant aisles and eliminates the usual back-order trigger for mixed configurations.
Finally, carrier scheduling plays a bigger role than most teams admit. Instead of waiting for the entire mixed pallet to be wrapped and labeled before calling the truck, the loading dock can stage low-profile boxes on one side and heavy-duty crates on the other, then merge them during the final scan. Having a designated mixed-order lane at the dock means the truck gets loaded in the same sequence as the pick list. The result is a single delivery that arrives complete, with no separate drop-offs or partial shipments slowing down the installation crew.
Pre-Shipment Inspection Data You Can Actually Use
Most pre-shipment inspection reports dump a pile of photos and a checklist on you, but the actual decision hinges on a handful of numbers. You need the count of cartons opened, the number of units checked, and the split between critical, major, and minor defects. Without that, you're just staring at a warehouse gate and hoping for the best.
The data becomes usable when it points to a location, not just a category. If five out of eight rejected pieces come from carton 14, that tells you something about a specific run or a specific operator. Pair those defect counts with measured dimensions for the top five risk points on your spec sheet, and you can tell a factory exactly what to rework before the container gets sealed.
A final field note for each failing check keeps everyone honest. If the note says carton 22, unit 7, gap between panel and frame at 2.1mm against a 1.5mm tolerance, that is far more useful than a vague note about workmanship issues. When the supplier replies, you want a corrective action plan that names a deadline and a person responsible, not a boilerplate promise to pay more attention.
Packaging That Survives Forklifts, Salt Air, and Tight Warehouses
Few things test packaging like a forklift driver in a hurry. The wrong box gets a tine through the side, a crushed corner, or a split seam that sends product spilling across the dock. We’ve seen standard corrugated fail within minutes under a careless clamp, so we build ours with reinforced edge crush ratings and double-wall fluting. Drop a pallet from waist height or let a 3,000-pound truck nudge it against a rack—the box should flex, not fracture. That means tighter glue patterns, stronger staples, and sometimes a simple but overlooked trick: rotating the flute direction so the vertical strength runs where the forks hit first.
Salt air is quieter but just as brutal. It works its way into paper fibers, softens adhesives, and leaves a white bloom on metal straps. For coastal warehouses or anything shipped across an ocean, we skip the standard starch-based glue and switch to moisture-resistant resins. We also wrap the pallet differently—not just a few turns of stretch film, but a full shroud that lets the load breathe without letting brine seep in. The goal is a package that arrives without rust-stained edges or swollen cardboard, even after weeks in a humid port.
Tight warehouses are the third enemy. Aisles measured in inches, racks packed to the ceiling, and drivers who need to make a three-point turn with a pallet that’s slightly too wide. Packaging that can’t stack cleanly jams the whole flow. So we design for modular footprints—boxes that sit flush on standard 48×40 pallets without overhang, and internal dividers that stop product from shifting when a pallet gets tilted on a ramp. The best packaging doesn’t just survive the hit; it makes the next forklift pass a little less risky.
FAQ
You get direct access to a huge manufacturing network that has specialized in casters for decades. Many factories in Ningbo and around the Yangtze Delta keep raw material inventories high, so they can turn orders faster and at a fraction of the cost you would see from distributors elsewhere.
Load ratings are tied to wheel material and bearing type, so a factory should show test data for static and dynamic loads, not just claim a number. Reputable manufacturers run jig tests at 1.5 to 2 times the rated load and inspect for deformation, bearing play, and thread integrity before signing off.
Yes, custom threads and top plate patterns are standard work for most Chinese caster factories. You send a drawing or even a rough sketch with key measurements, and they will modify existing molds or machine new stems. Setup fees for threads are usually low because they keep a wide range of taps and dies on hand.
Polyurethane on cast iron or nylon cores is common for floors that need protection and quiet rolling. Nylon wheels work well in wet or chemical environments but can be noisy on rough concrete. Rubber wheels give good grip and absorb shock but wear faster under heavy loads. Matching the material to your floor and load type avoids flat spots and floor damage.
Standard leveling casters with common specs often ship within 15 to 25 days after deposit. Fully custom stems or special plating can add 10 to 15 days. Sea freight to the US or Europe typically takes 20 to 35 days, so a realistic total is six to nine weeks door to door, though many factories hold stock for popular sizes.
Most will start with as few as 100 to 200 pieces per size if you accept standard packing, though the unit price drops sharply above 1,000. Mixed containers are normal, you can combine several wheel sizes and stem types in one shipment. A trial order is a smart way to verify finish quality and packaging before committing to a large run.
Beyond visual inspection, reliable factories check stem straightness with a dial gauge, test swivel action for binding, and measure wheel hardness with a durometer. For plated parts, they often run a salt spray test to catch rust issues early. You can also ask for an inspection report with photos and measurements for each batch.
Zinc plating is the baseline, but for humid or outdoor use, you can specify nickel or chrome plating on stems and brackets, or switch to stainless steel for critical parts. Many Chinese factories also offer a clear e-coat over zinc to extend corrosion resistance. Ask for the specific plating thickness in microns rather than accepting vague promises.
Conclusion
When you're sourcing leveling casters, the difference between a standard catalog part and one that actually fits your machine often comes down to how the factory handles the details. A China-based manufacturer that specializes in these components will look beyond the total load rating and check the exact footprint of your equipment. That matters because two machines can weigh the same but distribute force completely differently, and a caster sized only by weight may put too much pressure on a small mounting plate. Working directly with the engineering team also shortens the loop when something needs to change, whether that's a finer thread pitch for a metric mount or a softer wheel compound to protect a sensitive floor. You're not waiting on a distributor to relay a message; you can get a revised drawing or a sample in days. On top of that, leveling pads from a factory that understands real workshop conditions are designed to hold position on sloped or worn concrete, not just on a perfectly flat test bench.
The second reason is operational flexibility. A lot of equipment projects need a mix of low-profile casters for tight clearances and heavy-duty models for the main load-bearing points, and a dedicated factory can combine those in one order without delaying the whole shipment. You don't have to split the purchase between two suppliers or settle for a compromise size. Before anything leaves the dock, you should also receive pre-shipment inspection data that's actually useful: measured wheel hardness, thread gauge results, and load test photos rather than a generic certificate. And because the goods may travel by sea and sit in a crowded warehouse, the packaging has to be more than an afterthought. A factory that regularly exports to industrial buyers wraps each caster to survive forklift handling, salt air, and tight storage racks, so the parts arrive ready to install instead of needing cleanup or replacement.
Contact Us
Contact Person: Ruby
Email: [email protected]
Tel/WhatsApp: +86 13360379367
Website: https://www.cmcl-casters.com